VPSA biogas upgrading for anaerobic digestion, with methane purity up to 99% and near-total recovery from waste water and organic waste feedstock.

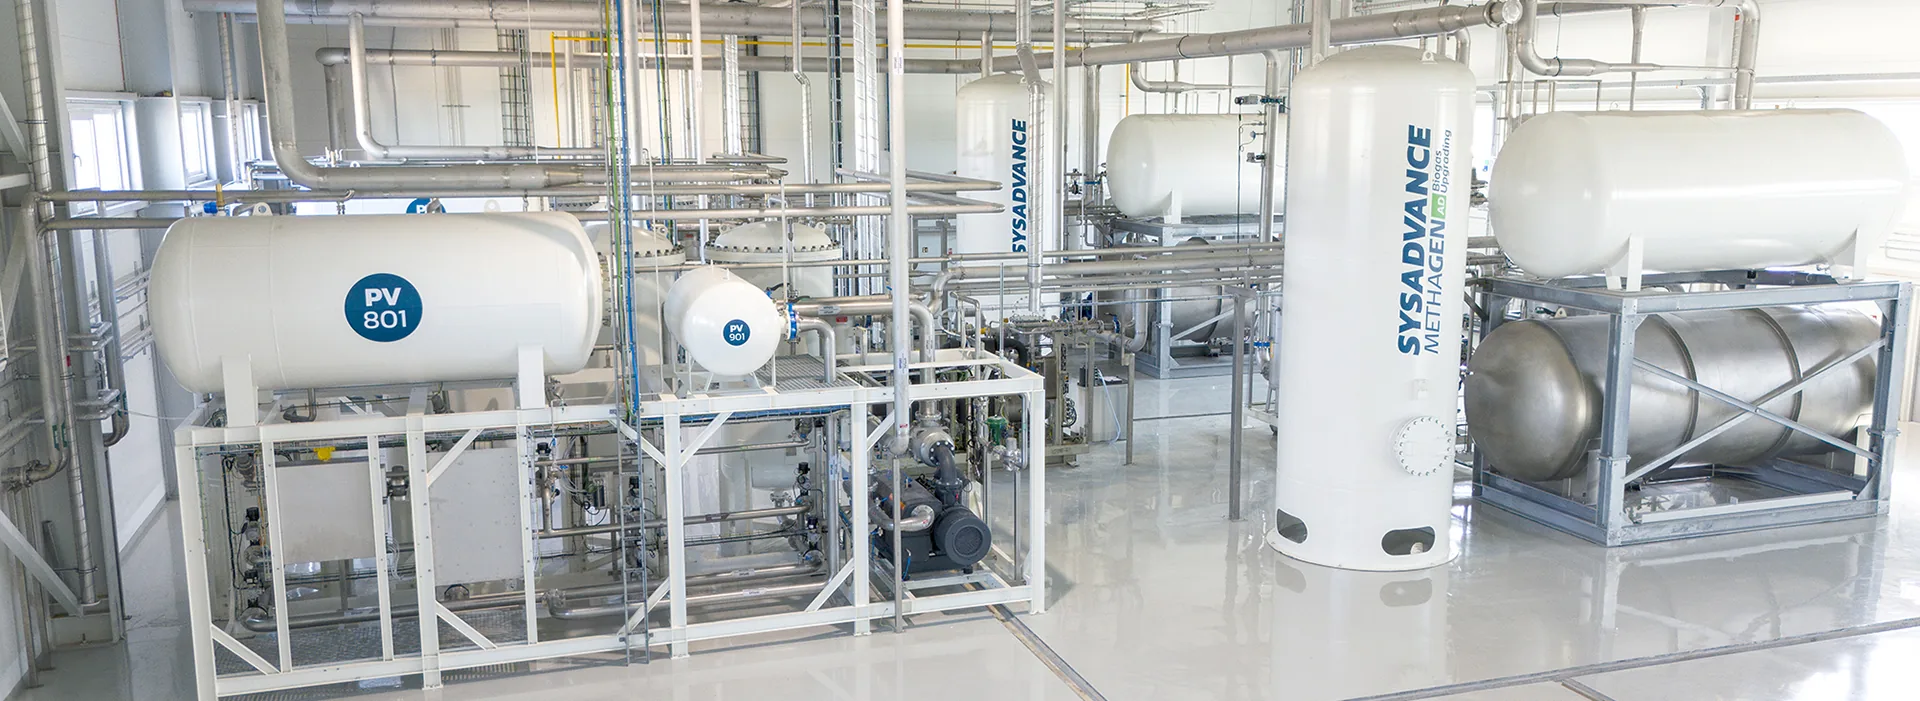
METHAGEN AD is a system, based on VPSA (Vacuum Pressure Swing Adsorption) technology designed to purify biogas from Anaerobic Digestion feedstock.
Typical feedstock includes waste water treatment plants, and food and organic municipal waste.
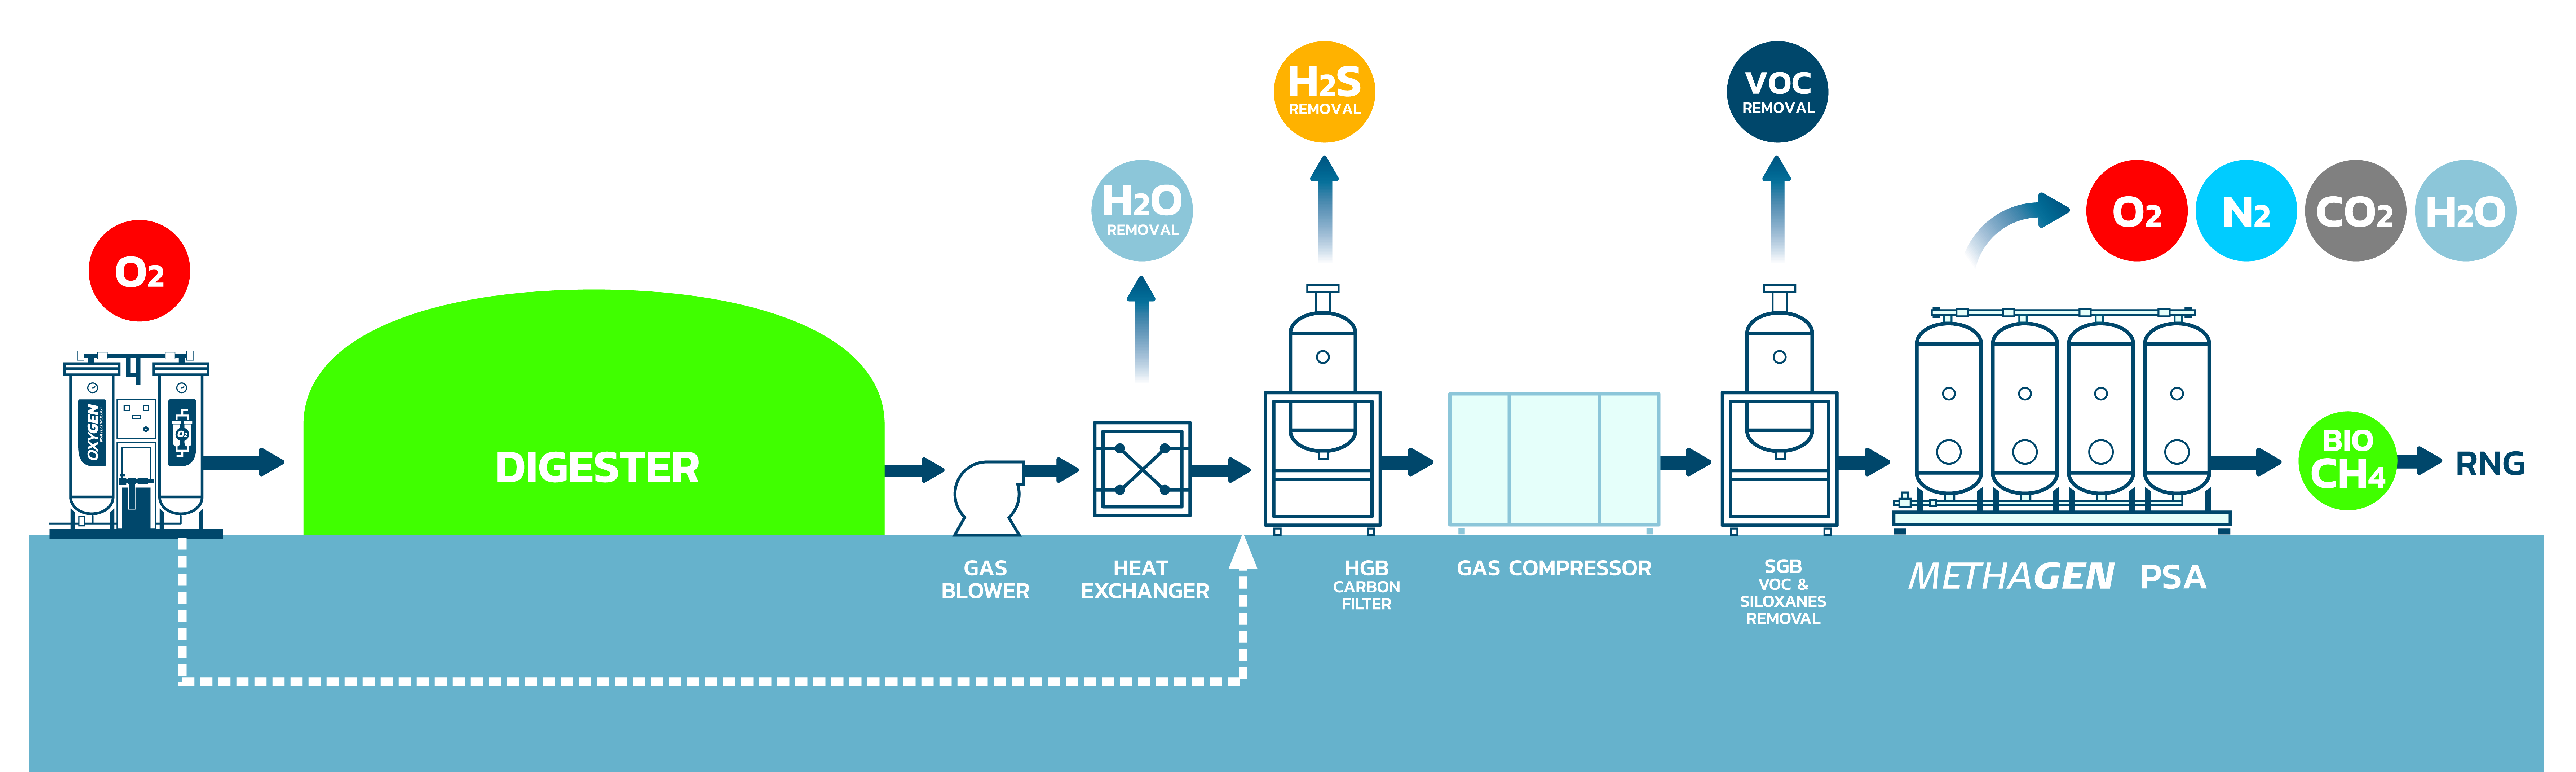
After being previously dried and desulphurized, compressed biogas is fed to the METHAGEN Upgrading Unit that makes use of VPSA technology to remove CO2, N2, O2 and residual H2O from the gas stream.

Achieve less than 1% Methane loss recovery, eliminating methane emissions and maximizing biomethane production.
Industry-leading efficiency with energy consumption as low as 0.18 kWh/Nm³ of biogas.
Reduce initial investment costs with an optimized and cost-effective upgrading solution.
Produce biomethane with methane purity levels of up to 99%.
Recover up to 99.5% of methane, ensuring maximum energy valorisation.
Non-cryogenic technology with no water or chemicals required, minimizing operating complexity.
Quick start-up and shutdown, high availability and simple installation for dependable performance.
Industry 4.0 enabled, remote monitoring, dynamic reporting and optional CO₂ recovery (CCU) in a complete turnkey system.
VPSA Technology
The METHAGEN system contains a set of columns packed with selective adsorbents. Each adsorption column undergoes a cyclic sequence of pressure steps, to produce a continuous flow of high-purity, dry and pressurized biomethane.
The adsorbent regeneration step is assisted by a vacuum system to enhance the process efficiency. The residual methane desorbed during the regeneration step is recycled back to the biogas inlet reservoir, resulting in a methane recovery rate close to 99%.
The METHAGEN operation is fully automated and controlled by a PLC. The biomethane composition is continuously monitored by a multi-gas analysis system.
Download our comprehensive brochure with detailed specifications, diagrams, and performance charts for our energy and biogas upgrading solutions.
Energy Catalogue
Download BrochurePressure Swing Adsorption (PSA) separates gases by taking advantage of the different adsorption characteristics of gas molecules under pressure. As compressed gas enters an adsorbent vessel, unwanted components are retained on the adsorbent while the desired product gas passes through.When the adsorbent becomes saturated, the vessel is depressurized to release the captured gases and regenerate the adsorbent. Multiple vessels operate in sequence so that purification and regeneration occur simultaneously, providing a continuous supply of high-purity gas.
Talk to EngineerA PSA system automatically regulates pressure, cycle timing, and gas flow to achieve the required purity and production rate. Modern PLC-based control systems continuously monitor operating conditions and adjust the cycle parameters to maintain stable performance despite changes in demand and inlet biogas composition
Talk to EngineerTurndown refers to the range over which a PSA can reduce its production while maintaining the specified gas quality. Depending on the process design, many PSA systems can operate efficiently across a wide flow range without compromising product purity.
Talk to EngineerGas purity depends on feed gas composition, pressure, temperature, flow rate, and adsorption cycle timing. Once commissioned, the PSA is optimized for its design conditions, but operating parameters are self-adjusted if process conditions change.
Talk to EngineerThe adsorbent material depends entirely on the application. Common materials include activated alumina, silica gel, molecular sieves (zeolites), and activated carbon. The selection is based on the target gas separation, contaminant levels, and operating conditions.
Talk to EngineerUnder normal operating conditions, PSA adsorbents typically provide many years of reliable service. Their lifetime depends largely on feed gas quality and correct operation. Exposure to liquid contaminants, excessive particulate loading, or operation outside design limits can reduce adsorbent performance. On average, if no serious contamination occurs, adsorbent is expected to last more than 10yrs.
Talk to EngineerPSA technology is widely recognized for its high reliability because it contains relatively few moving parts. With routine preventive maintenance and correct operating conditions, plant availability typically exceeds 99%, making PSA suitable for continuous industrial operation.
Talk to EngineerCommissioning time depends on system size and complexity. Smaller packaged systems are often operational within a few days, while larger industrial installations generally require one to two weeks, including testing, optimization, and operator training.
Talk to EngineerThe main operating costs are electricity for compressors and controls, routine maintenance, and periodic replacement of filters or consumable components. Since PSA systems require no chemical regenerants, operating costs are generally predictable and comparatively low.
Talk to EngineerRoutine maintenance generally includes replacing filter elements, inspecting valves and instrumentation, checking control systems, and performing scheduled servicing of rotating equipment where applicable. Following the manufacturer's maintenance schedule helps ensure long-term reliability.
Talk to EngineerElectrical requirements vary depending on system size and customer standards. PSA systems are available for a wide range of international voltages and frequencies and can be integrated with existing plant electrical infrastructure.
Talk to EngineerYes. Many PSA systems allow cycle parameters to be adjusted to accommodate moderate variations in feed gas composition, pressure, or required product purity. Significant process changes may require re-optimization by the equipment supplier.
Talk to EngineerResidual oxygen can create safety risks, increase corrosion and prevent compliance with gas grid specifications. METHAGEN VPSA directly removes oxygen without requiring a separate deoxygenation unit.
Talk to EngineerDepending on the application, oxygen levels as low as 0.2% can be achieved without additional DEOXO equipment.
Talk to EngineerDirect oxygen removal avoids additional deoxygenation equipment, reducing CAPEX, maintenance and OPEX, as well as to allow Oxygen injection in Biogas for H2S reduction.
Talk to EngineerYes. Oxygen may be injected upstream in the digestor or HsS filter system to improve H₂S removal while VPSA removes residual oxygen before grid injection, increasing efficiency in H2S reduction and decreasing costs associated with H2S pre-treatment.
Talk to EngineerNitrogen reduces biomethane calorific value and may prevent compliance with pipeline specifications.
??
Talk to EngineerYes. The METHAGEN LF VPSA process is specifically designed for efficient nitrogen removal up to 20% Nitrogen.
Talk to EngineerMembranes separate CO₂ efficiently but have limited methane/nitrogen selectivity, thus not allowing for the removal of Nitrogen in Biogas..
Talk to EngineerNo. It is effective but generally requires higher energy consumption and more complex and costly equipment.
Talk to EngineerAutomatic control adjusts cycle time and feed flow to maintain stable product quality.
Talk to EngineerYes. Continuous process control maintains biomethane quality, independently from volatility in Biogas inlet composition.
Talk to EngineerVPSA is generally more tolerant of temporary contaminant excursions than membrane systems.
Talk to EngineerSiloxanes, VOCs, ammonia, liquid water, compressor oil and particulates.
Talk to EngineerVPSA is less likely to suffer permanent damage than membrane systems after temporary upsets.
Talk to EngineerLower energy consumption reduces lifetime operating costs.
Talk to EngineerSpecific energy consumption can be as low as approximately 0.18 kWh/Nm³ under suitable conditions.
Talk to EngineerReduced electricity consumption lowers OPEX throughout the project lifetime.
Talk to EngineerTypically after around 10 years or longer under normal operating conditions.
Talk to EngineerVPSA generally requires fewer replacement interventions, reducing lifecycle costs.
Talk to EngineerNo. It is a dry adsorption process.
Talk to EngineerYes, subject to local gas quality specifications, up to 99% CH4 concentration.
Talk to EngineerYes. It builds on SYSADVANCE's extensive PSA installation base.
Talk to EngineerApproximately 165 to 5,000 Nm³/h in modular configurations.
Talk to EngineerA PSA can be integrated into a plant control system using standard industrial communication protocols and conventional digital or analog I/O. The exact signal list depends on the level of automation and customer requirements.
Talk to EngineerMost PSA systems reach operating pressure within minutes and begin producing gas shortly afterward. Full design purity is typically achieved once the adsorption cycle has stabilized.
Talk to EngineerDuring an emergency stop, feed gas is isolated and the adsorption cycle stops safely. Once the cause has been resolved, the system can normally be restarted following the standard operating procedure. Extended shutdowns may require depressurization before restart.
Talk to EngineerYes. Industrial PSA systems are commonly designed for outdoor installation and can be supplied with weather protection, insulation, heat tracing, or other environmental features to suit local climate conditions.
Talk to EngineerHigher feed pressure generally improves adsorption efficiency and reduces equipment size, provided the system operates within its design limits. The optimum operating pressure depends on the gas composition and the required product specifications.
Talk to Engineer

Need technical advice? Our engineering team is ready to help you define the best solution for your application.
Daniel Esteves
Sales Executive Energy Division


Ready to move forward? Request a detailed proposal tailored to your needs.